Nickel-based superalloys are engineered to withstand extreme operating conditions, including high mechanical stress, corrosive chemical environments, and elevated temperatures. However, raw material chemistry alone is not enough; the microstructure achieved through precise thermal processing dictates whether a component delivers decades of reliable service or fails prematurely.
Unlike carbon and low-alloy steels, nickel alloys are highly sensitive to thermal excursions. Mismanaged heating, soaking, or cooling cycles can destroy corrosion resistance, induce severe embrittlement, or warp expensive components.
1. Solid-Solution vs. Precipitation-Hardened Alloys: The Fundamental Logic
Before designing a thermal cycle, engineers must distinguish between the two primary metallurgical families of nickel alloys, as their strengthening mechanisms require entirely different heat treatment logic.
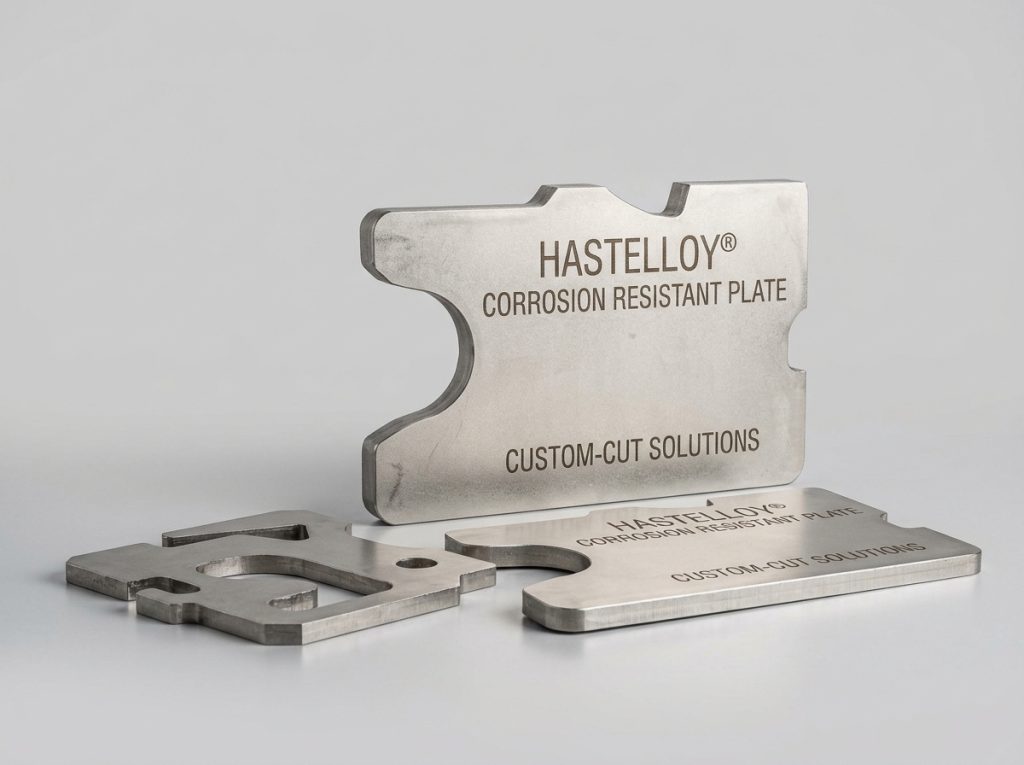
- Solid-Solution Strengthened Alloys (e.g., Alloy 625, Hastelloy C-276, Monel): These alloys derive their strength from alloying elements (such as molybdenum, chromium, and tungsten) dissolved in the nickel matrix. They cannot be hardened by heat treatment. Their thermal processing is strictly limited to solution annealing to dissolve secondary phases, homogenize grain structures, and relieve fabrication stresses. A clear example of this metallurgical split is evaluated in our breakdown of Alloy 625 vs. Alloy 718 key differences.
- Precipitation-Hardened (Age-Hardenable) Alloys (e.g., Alloy 718, Alloy X-750): These alloys contain additions of titanium, aluminum, or niobium that form fine, coherent secondary hardening phases ($\gamma’$ or $\gamma”$) during controlled aging cycles. They require a precise two-stage thermal sequence—solution annealing followed by aging—to achieve ultra-high tensile and yield strengths.
2. Solution Annealing: Restoring Homogeneity and Corrosion Resistance
Solution annealing is the cornerstone thermal treatment for nearly all wrought nickel alloys, whether they are solid-solution or precipitation-hardened.
- Purpose: The primary objective is to dissolve undesirable carbides, intermetallic phases (such as Laves or sigma phase) that may have precipitated during hot working or welding, and to relieve residual cold-working stresses.
- Temperature Control: Annealing must be conducted within a tightly controlled temperature window specified for each grade (typically between 980°C and 1230°C / 1800°F to 2250°F). Overheating leads to rapid grain coarsening, which degrades room-temperature mechanical properties and low-cycle fatigue resistance.
- Rapid Quenching: Following the soak period, rapid cooling (usually via water quenching or rapid forced-air cooling for heavier sections) is mandatory. Slow cooling through the critical sensitization range (550°C to 800°C) allows carbides to reprecipitate at grain boundaries, destroying corrosion resistance.
3. Precipitation Hardening (Aging): Unlocking Maximum Strength
For age-hardenable alloys like Alloy 718, solution annealing merely sets the stage. The component is still in a relatively soft, formable condition after annealing.
- The Aging Cycle: Aging involves holding the material at lower, intermediate temperatures (often a two-step cycle, e.g., 720°C followed by 620°C with controlled furnace cooling) to precipitate nanoscale intermetallic particles uniformly throughout the matrix.
- Dislocation Pinned Structure: These fine precipitates act as physical barriers to dislocation movement, drastically increasing yield strength.
- Dimensional Stability: Because aging temperatures are relatively low compared to solution annealing, components experience minimal distortion during the hardening stage, allowing near-net-shape machining prior to final aging.
4. Common Heat-Treatment Mistakes & Performance Degradation
Even minor deviations in furnace parameters can trigger catastrophic metallurgical failure. Fabrication shops must avoid these frequent pitfalls:
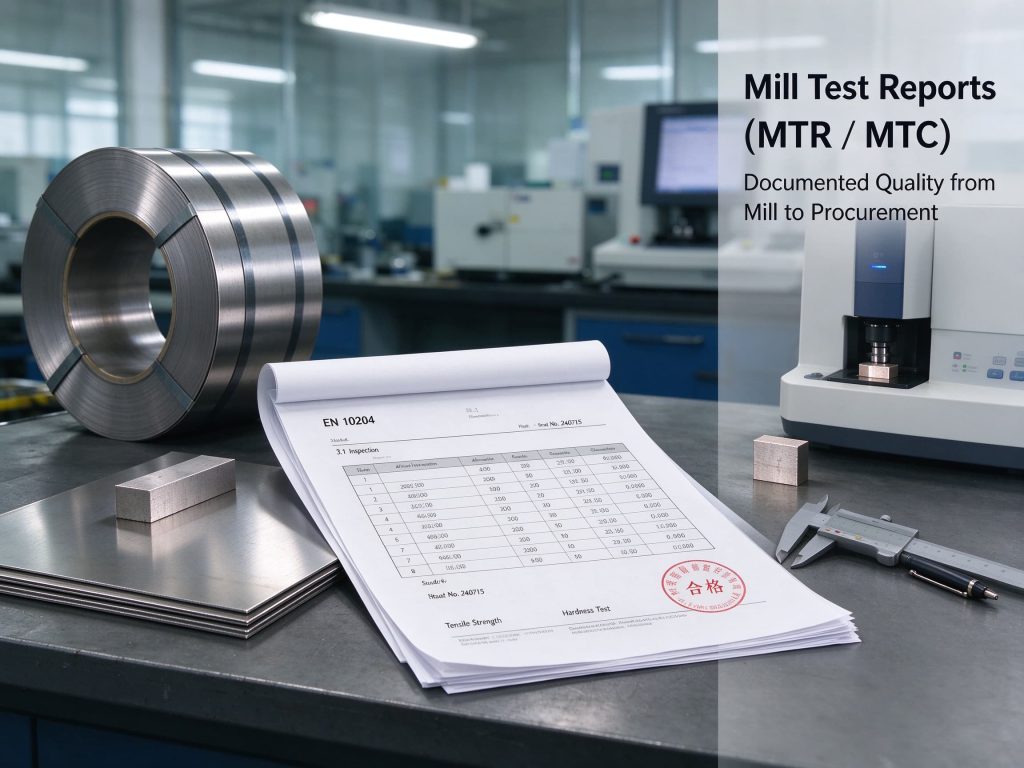
- Sensitization and Intergranular Attack (IGAs): Slow cooling or prolonged exposure in the 600°C–800°C range causes chromium carbides ($M_{23}C_6$) to precipitate along grain boundaries. This depletes adjacent matrix zones of chromium, creating localized galvanic cells that lead to rapid intergranular stress corrosion cracking (IGSCC) in service. Procurement teams can mitigate raw material risks by enforcing strict mill testing guidelines outlined in nickel alloy procurement quality checks.
- Formation of Embrittling Topological Close-Packed (TCP) Phases: Phases like sigma, mu, and Laves form when alloys are held at improper intermediate temperatures. These brittle phases severely reduce impact toughness and ductility, causing parts to shatter under unexpected mechanical shock.
- Furnace Atmosphere Contamination: Heating nickel alloys in sulfur-bearing furnace atmospheres (from dirty fuel oil, residual cutting fluids, or uncleaned brickwork) causes liquid metal embrittlement and catastrophic sulfur attack, destroying the surface alloy matrix. Neutral or reducing protective atmospheres (or vacuum furnaces) are heavily recommended.
5. Summary Best Practices for Fabrication Shops
- Verify Specifications: Always consult the ASME Boiler and Pressure Vessel Code (BPVC) or ASTM standards for exact soak times and temperature tolerances.
- Clean Before Heating: Completely degrease and remove all grease, paint, tape, and machining lubricants prior to putting parts into any furnace. Residual carbon reacts with nickel at high temperatures.
- Calibrate Pyrometry: Ensure furnace thermocouples and recording instruments undergo regular calibration to prevent thermal runaways or soak inaccuracies.